.png)
Author | SHENGWO Industry Insights Team
Updated | November 2026
Contents
In sheet metal fabrication, welding quality is about more than creating a strong joint.
The welding process can also affect dimensional accuracy, surface appearance, structural stability, and final assembly. Even a properly executed weld may create downstream problems if the component design, welding sequence, fixture arrangement, or finishing requirements have not been considered in advance.
For OEM manufacturers and industrial buyers, identifying potential welding risks before production can help reduce rework, improve manufacturing consistency, and avoid unnecessary delays.
So, what should engineers and manufacturers check before starting a sheet metal welding project?
Here are five important manufacturing risks to consider during the design and production planning stages.
Thermal distortion is one of the most common challenges in sheet metal welding.
During welding, localized heat causes the metal to expand. As the material cools, it contracts. Uneven heating and cooling can create residual stresses, resulting in warping, twisting, angular distortion, or dimensional changes.
This is particularly important for thin sheet metal components, large panels, frames, and welded structures that require precise alignment.
Before production, manufacturers should evaluate material thickness, joint configuration, welding sequence, and fixture support.
Depending on the component design, practical measures may include:
Engineering Tip: Do not assume that adding more weld material will automatically create a better structure. Excessive weld size can increase heat input, distortion, and finishing work without providing meaningful functional benefits.
A joint may look straightforward in a 3D model but become difficult to weld once the components are assembled.
Limited access can make it difficult for operators to position the welding torch correctly, maintain a consistent welding angle, or achieve the required weld profile.
This can affect both weld quality and production efficiency.
Common design problems include:
Welding accessibility should be reviewed during the design-for-manufacturing stage.
Engineers should consider:
Engineering Tip: Review the welding sequence alongside the 3D assembly model. A small adjustment to component spacing or joint positioning may prevent significant production difficulties later.
Welding fixtures are used to locate, support, and hold components during welding.
Their purpose is not simply to prevent parts from moving. A well-designed fixture helps maintain the correct relationship between components and supports repeatable manufacturing.
However, inaccurate locating points or excessive clamping force can create new problems.
For custom sheet metal assemblies, these issues may lead to incorrect hole positions, uneven gaps, frame misalignment, or dimensional deviations.
Before releasing a project for production, manufacturers should review:
It is also important to consider how the component will behave after it is released from the fixture. Clamping can temporarily hold a distorted part in position, but residual stress may cause movement after unclamping.
Engineering Tip: Verify critical dimensions after welding and fixture release, not only while the component is clamped.
Welding is often followed by grinding, polishing, or other finishing operations.
These processes may be required to remove excess weld material, smooth transitions, eliminate sharp edges, or prepare a surface for subsequent coating.
However, inconsistent grinding can create visible marks, uneven surfaces, excessive material removal, or damage to surrounding areas.
This is especially important for products where appearance matters, such as supermarket shelving, visible equipment panels, stainless steel components, and decorative metal structures.
Manufacturers should define finishing requirements before production begins.
Important considerations include:
Not every weld needs to be ground flush. Removing unnecessary weld material may weaken the joint or increase processing time.
Engineering Tip: Clearly identify visible surfaces and required finishing levels on drawings or approved samples. This helps prevent misunderstandings between engineering, production, and quality inspection teams.
A welded component may meet its individual manufacturing dimensions but still fail to fit correctly during final assembly.
This can happen because of welding distortion, inaccurate positioning, fixture issues, or tolerance accumulation across multiple components.
For example, a welded equipment frame may have the correct overall dimensions but still cause problems if mounting holes are misaligned or connection surfaces are not sufficiently flat.
Before mass production, manufacturers should identify critical interfaces and confirm how welded parts connect with other components.
Recommended checks include:
Engineering Tip: For complex welded structures, a first-article inspection or trial assembly can reveal fit problems before the full production batch begins.
A structured review before production can help engineers identify problems while design changes are still relatively easy to make.
| Risk Area | Key Questions Before Production | Recommended Action |
|---|---|---|
| Thermal distortion | Could heat input affect flatness or alignment? | Review welding sequence and heat input |
| Weld accessibility | Can every joint be reached properly? | Check 3D structure and welding clearance |
| Fixture accuracy | Are locating points and clamping positions reliable? | Review fixture design and references |
| Grinding marks | Which surfaces require finishing? | Define appearance and grinding requirements |
| Assembly mismatch | Will welded parts fit their mating components? | Check critical dimensions and trial assembly |
This review should be based on the approved engineering drawings, material specifications, weld requirements, and final application.
For complex projects, it is also useful to review the production sequence with engineering, welding, and quality teams before releasing the design for mass production.
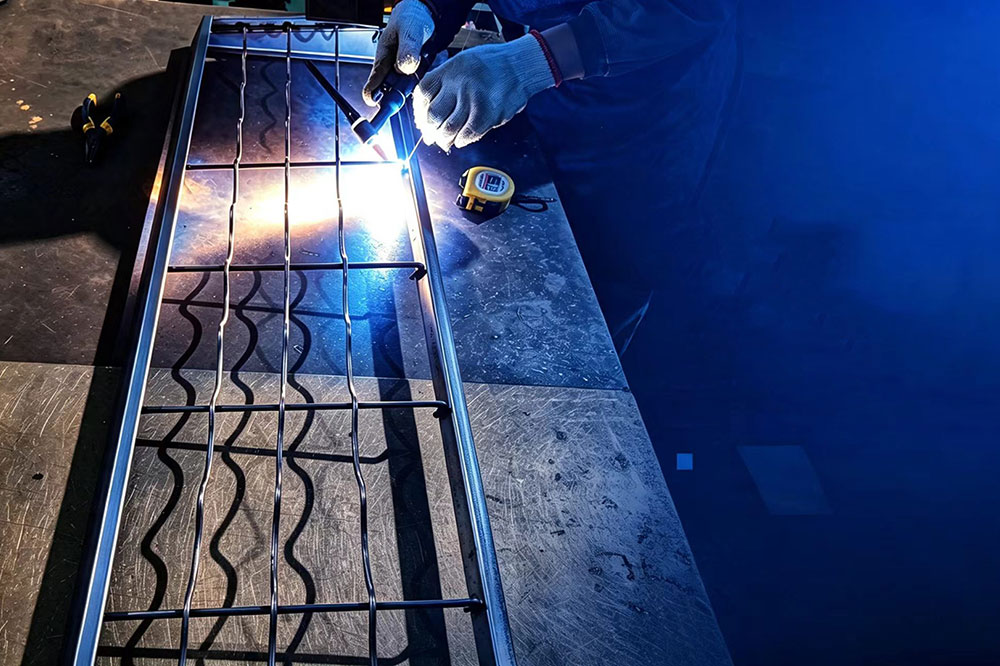
At SHENGWO MACHINERY, we provide custom sheet metal fabrication and metal component manufacturing for OEM customers across different industrial applications.
Our manufacturing scope includes custom supermarket shelving, HVAC dampers, equipment enclosures, electrical panels, and other sheet metal structures.
From engineering drawing review and laser cutting to CNC bending, welding, surface treatment, and final inspection, we focus on manufacturing details throughout the production process.
For custom sheet metal welding projects, important considerations include:
We believe that good welding quality starts before the first weld is made. Early engineering review and practical manufacturing planning help reduce avoidable problems during production.
Common risks include thermal distortion, poor weld accessibility, inaccurate fixture positioning, inconsistent grinding, and final assembly mismatch. These issues can affect product dimensions, appearance, structural integrity, and manufacturing efficiency.
Manufacturers can reduce welding distortion by controlling heat input, planning a balanced welding sequence, using suitable fixtures, selecting appropriate joint designs, and checking dimensions after welding. The correct approach depends on material thickness, geometry, and welding requirements.
Poor weld accessibility can restrict torch movement and make it difficult to maintain consistent welding conditions. Reviewing joint locations, component spacing, and assembly sequence during design helps improve both weld quality and production efficiency.
No. Grinding requirements depend on joint design, structural requirements, appearance expectations, and subsequent finishing processes. Unnecessary grinding can remove too much material, weaken a joint, or increase production costs.
Post-weld machining may be necessary when welded components have precision interfaces, tight dimensional requirements, or surfaces that must meet specific flatness or alignment criteria. It should be evaluated during manufacturing planning.
Buyers should ideally provide 2D engineering drawings, 3D STEP files, material grades and thicknesses, welding requirements, surface finishing specifications, critical tolerances, order quantities, and intended applications. This information helps manufacturers evaluate feasibility and prepare a more accurate quotation.
Successful sheet metal welding requires more than selecting a welding process and joining two metal components.
Thermal distortion, weld accessibility, fixture accuracy, grinding quality, and assembly compatibility should all be considered before production begins.
By identifying these five manufacturing risks early, engineers and manufacturers can reduce rework, improve dimensional consistency, and make the production process more predictable.
At SHENGWO MACHINERY, we combine engineering drawing review with custom sheet metal fabrication and manufacturing process planning to support OEM projects from design review to finished components.
Planning a custom sheet metal welding project?
Send us your drawings, 3D STEP files, material specifications, and estimated quantities for a manufacturing review and quotation.
SHENGWO MACHINERY — From Your Drawings to Reliable Manufactured Parts.
No. 8803 Zhuhai Road, LianWan Industry Park, Jinwan District, 519090 Zhuhai, Guangdong, China